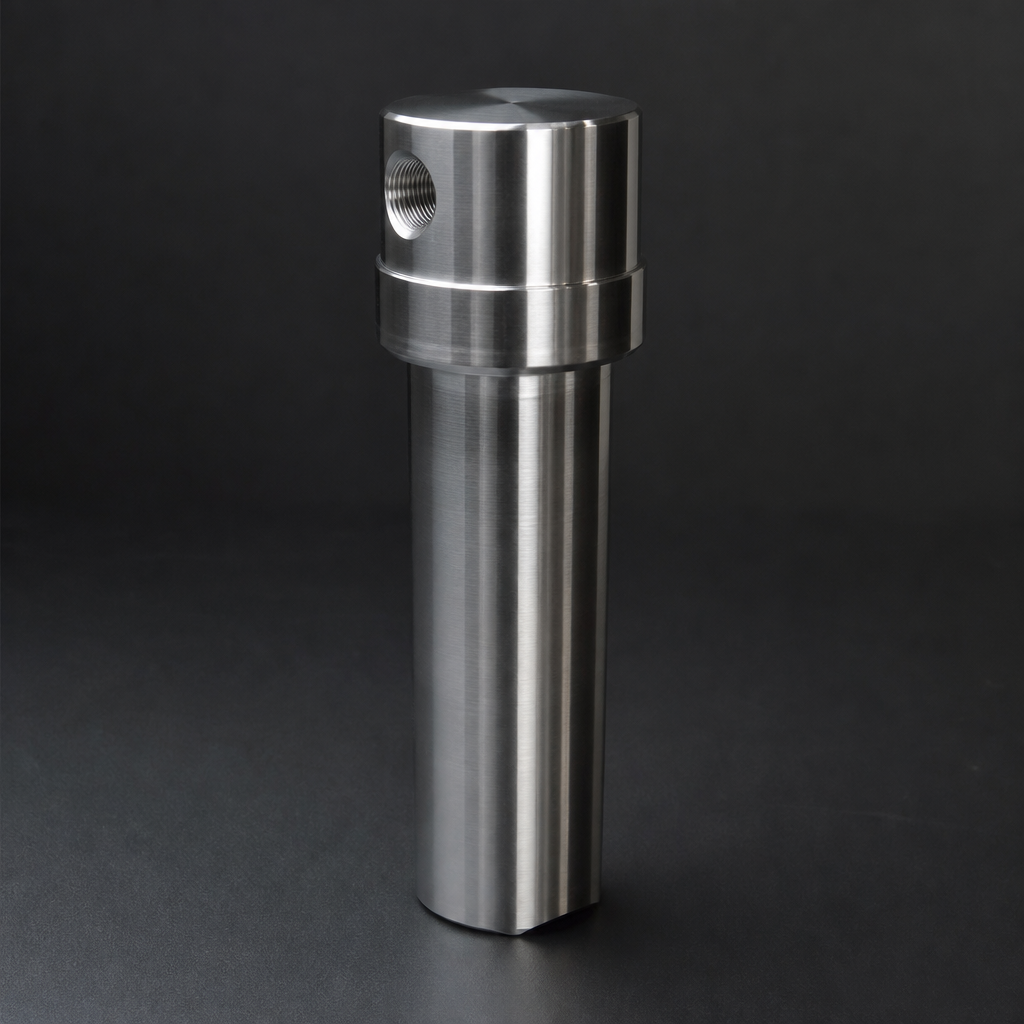
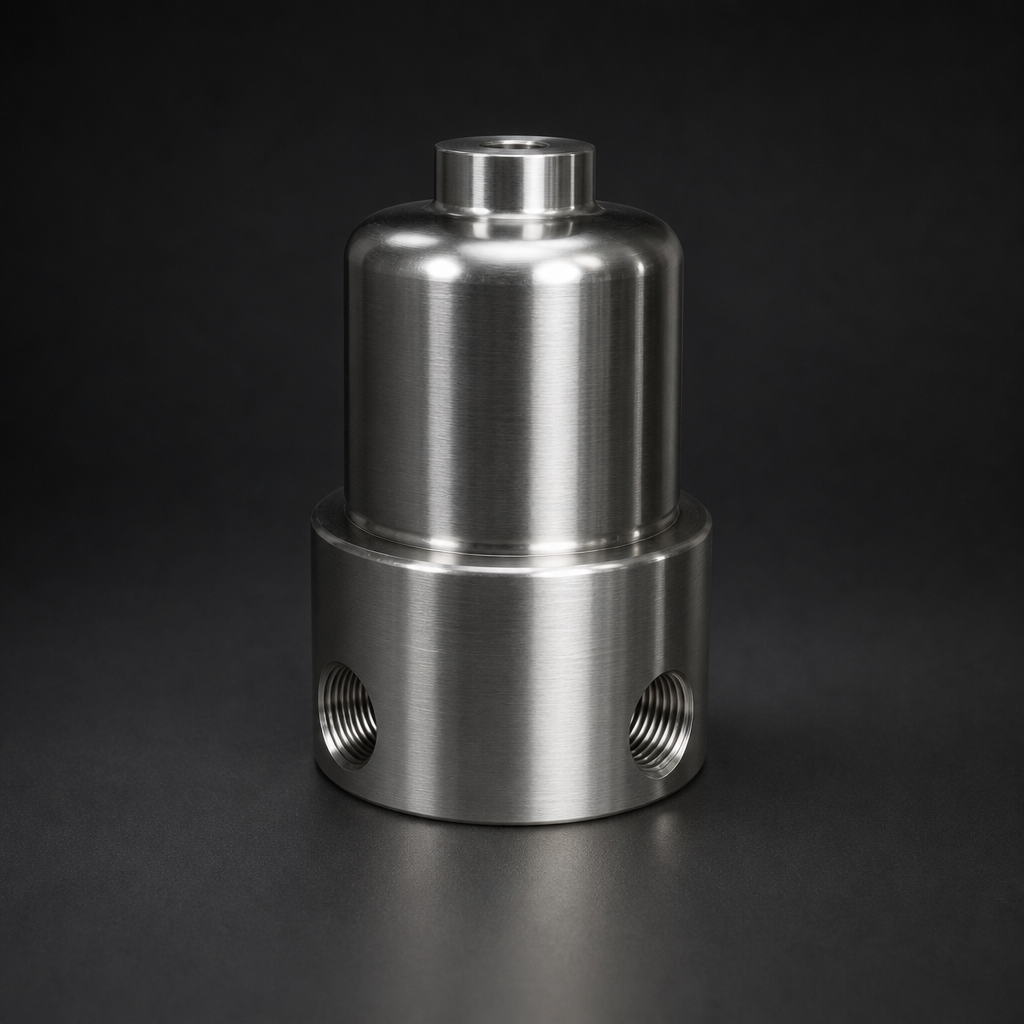
Liquid carry-over is one of the most damaging — and most preventable — failure modes in process analyser systems. When condensate, entrained droplets, or slug flow reaches a sensitive analyser, the consequences range from fouled sample cells and blocked capillaries to complete instrument failure and unplanned shutdowns. Float valve filter housings exist precisely to stop this from happening, providing an automatic, mechanical last line of defence between the sample stream and the instrument.
Why Liquid Carry-Over Happens in Analyser Sample Systems
Process streams are rarely as clean as they appear on a P&ID. Even gases that are nominally dry can carry significant liquid loads under certain conditions: temperature drops along sample lines, pressure let-down across regulators, and slug flow from upstream upsets all introduce liquid into what should be a vapour-phase sample. Conventional coalescing filters remove aerosols and fine mist effectively, but they are not designed to handle bulk liquid slugs. When a slug arrives, a standard filter element becomes saturated almost instantly, and liquid passes straight through to the analyser.
Common sources of liquid carry-over in analyser sample systems include:
- Condensation in unheated or poorly traced sample lines
- Upstream process upsets causing slug flow
- Inadequate knock-out capacity in the sample conditioning system
- Rapid pressure changes that cause retrograde condensation
- Failure of upstream coalescing stages
How Float Valve Technology Works
A float valve housing combines a conventional filter body with an internal float mechanism. Under normal dry-gas operation, the float sits at the bottom of the liquid collection chamber and the sample flows freely through the filter element to the analyser. As liquid accumulates in the sump, the float rises with the liquid level. When the liquid reaches a pre-set threshold, the float triggers one of two protective actions depending on the housing configuration:
- Automatic drain: The float opens a drain valve, discharging accumulated liquid to a safe collection point without interrupting sample flow.
- Flow shut-off / alarm: The float actuates a switch or closes the sample line, triggering an alarm at the control system and preventing any liquid from reaching the analyser.
The float mechanism is entirely passive — it requires no power, no control signal, and no operator intervention to function. This makes it inherently reliable in remote or unmanned installations where active monitoring may be limited.
Material Selection: Stainless Steel vs Polymer
Float valve housings are available in two primary material families, each suited to different service conditions. Selecting the wrong material is a common source of premature failure and sample contamination.
| Parameter | 316L Stainless Steel | PVDF / Polymer |
|---|---|---|
| Max. pressure | Up to 400 bar | Up to 10 bar |
| Temperature range | −60 °C to +200 °C | 0 °C to +80 °C |
| Chemical resistance | Excellent (most process gases) | Excellent (acids, solvents) |
| Typical application | Refinery, petrochemical, HP gas | Laboratory, low-pressure utility |
| Extractables risk | Negligible | Low (material-dependent) |
For the majority of process gas and refinery analyser applications, 316L stainless steel is the preferred choice. It handles the pressure and temperature ranges encountered in most sample conditioning systems, resists corrosion from H₂S, CO₂, and light hydrocarbons, and introduces no extractables that could interfere with trace-level measurements.
Need help selecting the right analyser protection filter?
The RF-H-170: Analyser Protection at Up to 400 Bar
The RF-H-170 analyser protection filter housing from R+F FilterElements is designed specifically for high-pressure sample conditioning service. Constructed from 316L stainless steel with a rated working pressure of 400 bar, it is suitable for the most demanding upstream oil and gas, refinery, and high-pressure process gas applications.
Key features of the RF-H-170 include:
- Integrated float valve mechanism for automatic liquid level detection and alarm actuation
- Compatible with RF-DIL disposable inline filter elements for particulate removal
- Available with FKM or PTFE seals for compatibility with aggressive process streams
- Compact body designed for installation in space-constrained analyser shelters
- Optional SilcoNert coating for ultra-trace and semiconductor-grade applications
Use our free Engineering Tool to get a filtration recommendation for your specific application in under 2 minutes.
Integrating Float Valve Housings into a Sample Conditioning System
Float valve housings are most effective when positioned correctly within the sample conditioning train. The recommended location is immediately upstream of the analyser, after any pressure let-down regulators and primary coalescing stages. This placement ensures that the float valve sees the final, conditioned sample stream and provides protection against any residual liquid that has passed through earlier stages.
For a complete analyser sample contamination prevention strategy, consider the following layered approach:
- Primary knock-out: A large-volume separator or cyclone at the sample tap to remove bulk liquid slugs before they enter the sample line.
- Coalescing filtration: An RF-DIL or similar coalescing element to remove aerosols and fine mist from the gas phase.
- Float valve housing: The RF-H-170 or equivalent, positioned as the final guard before the analyser, to catch any residual liquid and trigger an alarm if liquid levels become significant.
This three-stage approach provides defence in depth. Each stage handles a different liquid load and failure mode, so that no single component failure results in liquid reaching the analyser. For guidance on sizing each stage, the R+F Engineering Sizing Tool can assist with flow calculations and element selection.
Alarm Integration and Maintenance Considerations
Float valve housings with alarm output require integration into the plant DCS or local alarm panel. The float switch typically provides a dry contact output that can be wired to any standard digital input. When the float triggers, the recommended response sequence is:
- Isolate the analyser from the sample stream using the upstream isolation valve
- Drain the float valve housing sump to a safe collection point
- Investigate the upstream cause of the liquid carry-over before returning the analyser to service
- Inspect and replace the filter element if it has been saturated with liquid
Routine maintenance intervals for float valve housings in clean process gas service are typically 6–12 months, aligned with the element replacement schedule. In services with high liquid loads or frequent upsets, quarterly inspection is advisable. The instrumentation filter range from R+F FilterElements includes replacement elements compatible with the RF-H-170 housing.
For applications where the sample gas contains H₂S or other aggressive components, K-type elements with enhanced chemical resistance should be specified. These are available as part of the R+F filter element range and are drop-in compatible with the RF-H-170 housing body.
- Process streams are rarely as clean as they appear on a P&ID.
- Flow shut-off / alarm:
- Float valve housings are available in two primary material families, each suited to different service conditions.
- The RF-H-170 analyser protection filter housing from R+F FilterElements is designed specifically for high-pressure sample conditioning service.
Related Reading
- Coalescing vs Particulate Filter Elements — Which Do You Need?
- Oxygen Filtration Safety — Avoiding Ignition Risks in High-Purity Systems
- ISO 8573-1 Compressed Air Quality — A Practical Guide
Try our Engineering Sizing Tool → or discuss your requirements with our team.