Porosity, spatter, and weld oxidation are among the most frustrating defects in MIG and TIG welding — and contaminated shielding gas is a leading cause that is frequently overlooked. When moisture, particulate, or oil vapour enters the shielding gas stream, the protective envelope around the weld pool is compromised, allowing atmospheric oxygen and nitrogen to react with the molten metal. The result is costly rework, failed inspection, and in critical applications, structural failure. Point-of-use filtration at the welding station is the most direct and reliable solution.
Why Shielding Gas Purity Matters
Shielding gases — typically argon, CO₂, or blends such as Ar/CO₂ or Ar/He — serve a critical function: they displace atmospheric gases from the weld zone, preventing oxidation and nitridation of the molten pool. Any contamination in the gas supply directly undermines this protection. The three main contaminants are:
- Moisture (H₂O vapour): Causes hydrogen porosity, particularly in aluminium and austenitic stainless steel. Even 50–100 ppm moisture can produce visible porosity in TIG welds on aluminium.
- Particulate: Solid particles from cylinder valves, hose degradation, or regulator wear can block torch orifices, cause arc instability, and introduce inclusions into the weld pool.
- Oil vapour: Compressor oil carry-over in mixed-gas systems or from contaminated cylinders introduces carbon into the weld, causing porosity and reducing corrosion resistance in stainless steel.
The contamination source is rarely the bulk gas itself — certified industrial-grade argon and CO₂ are produced to tight purity specifications. The problem typically originates in the distribution system: ageing hoses, corroded fittings, moisture ingress at connections, or particulate shed from cylinder valves and regulators. This is why point-of-use inline filtration at the welding station is so effective — it addresses contamination introduced downstream of the cylinder, where it is most likely to occur.
The Impact on Weld Quality
The consequences of contaminated shielding gas manifest in several ways, each with direct cost implications:
Porosity is the most common defect linked to gas contamination. In structural steel fabrication, porosity above the limits set by EN ISO 5817 or AWS D1.1 requires weld repair or rejection — adding significant cost and schedule delay. In aerospace and pressure vessel applications, the tolerances are even tighter, and a single contamination event can result in scrapping an entire weld run.
Spatter increases when arc stability is disrupted by particulate or moisture. Excessive spatter means more post-weld cleaning, higher consumable consumption, and increased risk of surface defects. In automated MIG welding lines, spatter build-up on torch nozzles is a leading cause of unplanned downtime.
Oxidation and discolouration — the "sugaring" seen on the back face of stainless steel TIG welds — is a direct indicator of inadequate shielding. While sometimes attributed to insufficient back-purge gas, contaminated shielding gas at the torch can produce the same effect, reducing corrosion resistance and requiring mechanical or chemical remediation.
Point-of-Use Filtration: The Practical Solution
Installing a disposable inline filter directly at the welding station — between the regulator/flowmeter and the torch hose — is the most cost-effective intervention. These compact filters require no tools to install, no maintenance, and are replaced periodically as part of routine consumable management.
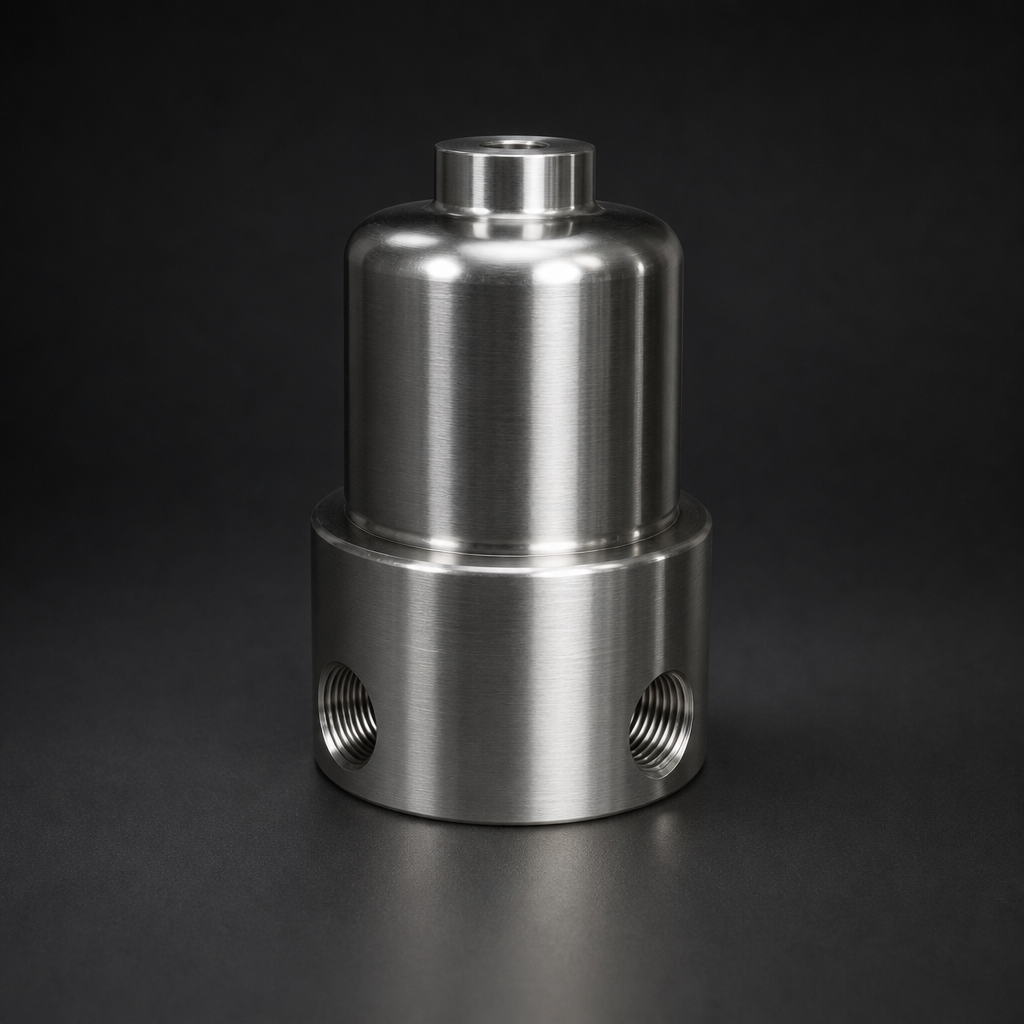
The RF-DIL disposable inline filter, available from R+F FilterElements, is designed specifically for this application. It removes particulate down to 0.1 µm, protecting the torch and weld pool from solid contamination introduced anywhere in the gas distribution system. Its compact body fits inline with standard 3/8" BSP or G1/4" connections used on most welding regulators and flowmeters.
Need help selecting the right filter for your welding application?
Use our free Engineering Tool to get a filtration recommendation for your specific application in under 2 minutes.
Selecting the Right Filter Configuration
The appropriate filter configuration depends on the base material, welding process, and gas supply arrangement. The table below summarises recommended configurations for common welding scenarios:
| Application | Gas | Primary Risk | Recommended Filter |
|---|---|---|---|
| MIG welding, mild steel | Ar/CO₂ (75/25) | Particulate, spatter | RF-DIL (point-of-use) |
| TIG welding, aluminium | Pure Ar | Moisture, particulate | RF-H-150 + RF-C + RF-DIL |
| TIG welding, stainless steel | Ar or Ar/He | Moisture, oil vapour | RF-H-150 + RF-C + RF-AC + RF-DIL |
| Automated MIG line | Ar/CO₂ blend | Particulate, arc instability | RF-DIL per station |
| Orbital TIG, tube/pipe | Pure Ar (99.999%) | All contaminants | RF-H-150 + RF-C + RF-DIL |
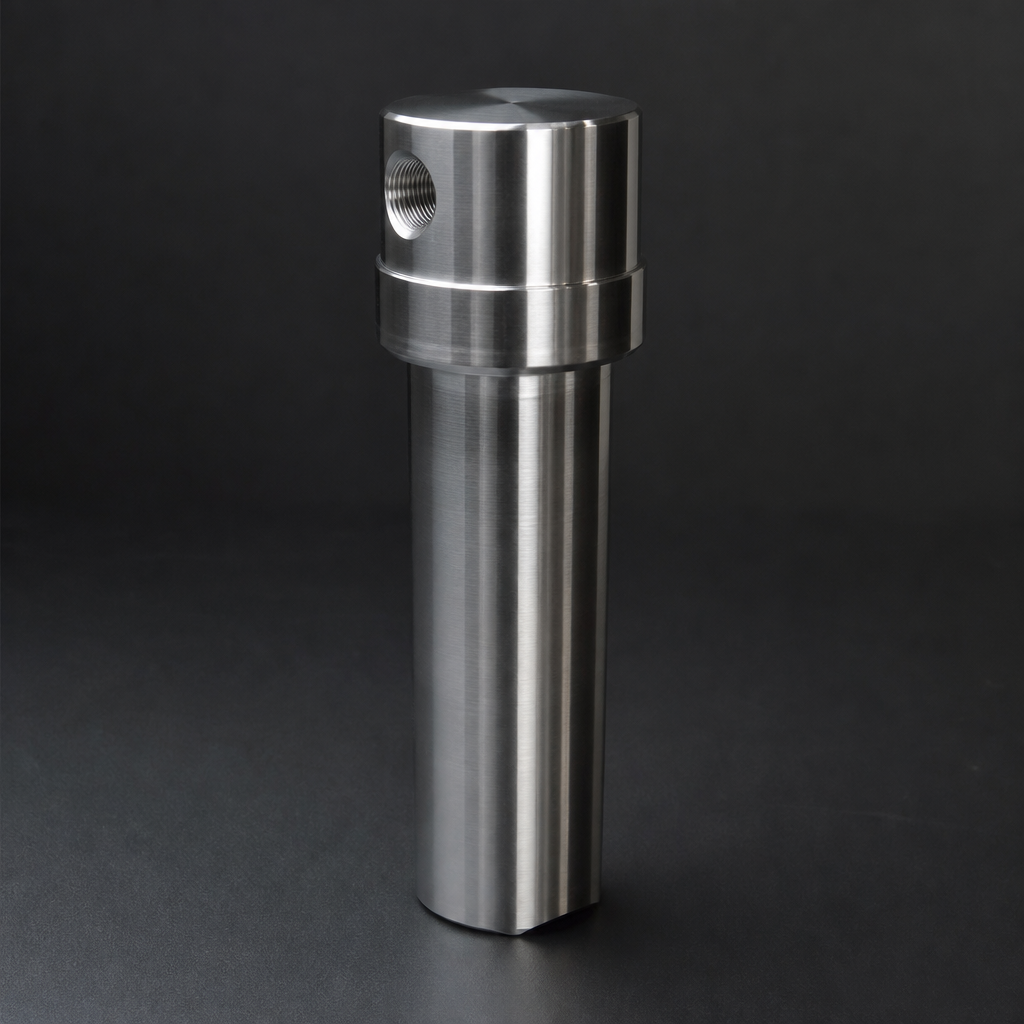
For centralised gas supply systems serving multiple welding stations, a process gas housing such as the RF-H-150 installed at the manifold provides bulk filtration, with RF-DIL units at each individual station providing final point-of-use protection. This two-stage approach is particularly effective in large fabrication shops where long hose runs increase the risk of particulate ingress.
Integration with Welding Quality Systems
Modern welding quality management systems — particularly those operating under EN ISO 3834 or ASME Section IX — require documented control of all variables that affect weld quality, including shielding gas purity. Installing and recording the use of point-of-use filtration provides a straightforward, auditable control measure that satisfies this requirement.
For manufacturers supplying to the aerospace, nuclear, or pressure equipment sectors, where gas purity standards are strictly enforced, documented filtration at the point of use is increasingly expected by third-party auditors. The RF-DIL and RF-H-150 series are compatible with standard quality documentation practices and can be referenced in welding procedure specifications (WPS) and procedure qualification records (PQR).
It is also worth noting that shielding gas filtration complements — but does not replace — other gas quality controls such as cylinder certification, regulator maintenance, and hose inspection. A comprehensive gas quality programme addresses all potential contamination sources. For guidance on broader filter element selection and process gas applications, R+F FilterElements provides application engineering support.
- Moisture (H₂O vapour):
- The consequences of contaminated shielding gas manifest in several ways, each with direct cost implications:
- Installing a disposable inline filter directly at the welding station — between the regulator/flowmeter and the torch hose — is the most cost-effective intervention.
- The appropriate filter configuration depends on the base material, welding process, and gas supply arrangement.
Practical Implementation
Implementing point-of-use shielding gas filtration is straightforward. The RF-DIL installs in seconds using standard push-fit or threaded connections. No tools, no bypass valves, no pressure drop concerns for typical welding flow rates (5–25 l/min). Replacement intervals depend on gas quality and usage, but in most fabrication environments, a quarterly replacement schedule is sufficient.
For high-volume automated lines or applications with known gas quality issues, a more structured approach is recommended: install an RF-H-150 housing with a coalescing RF-C element at the cylinder manifold, followed by RF-DIL units at each welding station. This configuration provides comprehensive protection across the entire gas distribution system and is the approach recommended by R+F FilterElements for critical welding applications.
Related Reading
- Coalescing vs Particulate Filter Elements — Which Do You Need?
- ISO 8573-1 Compressed Air Quality Classes Explained
- Oxygen Filtration Safety — What Every Engineer Must Know
Try our Engineering Sizing Tool → or discuss your requirements with our team.