Why Inert Gas Purity Is Critical in Metal Additive Manufacturing
Selective Laser Melting (SLM) and Direct Metal Laser Sintering (DMLS) have transformed precision component production — but both processes are acutely sensitive to atmospheric contamination. During a build, the laser melts metal powder at temperatures exceeding 1,500 °C, generating metal condensate, spatter particles, and soot that immediately contaminate the inert gas atmosphere inside the build chamber. If these contaminants are not removed continuously, they scatter the laser beam, degrade part density, and introduce porosity that compromises mechanical integrity.
For engineers specifying filtration systems for additive manufacturing cells, the challenge is not simply removing particles — it is maintaining ISO 8573-1 Class 1 purity in a recirculating gas loop at high flow rates, with minimal pressure drop, and without introducing any moisture or hydrocarbon contamination that could oxidise the metal powder or affect the melt pool chemistry.
The Contamination Profile in SLM and DMLS Build Chambers
Understanding what you are filtering is the first step to specifying the right system. Metal additive manufacturing generates a distinctive contamination mix:
- Metal condensate (fume): Sub-micrometre particles (0.1–1 µm) formed when vaporised metal re-solidifies. These are the most penetrating contaminants and require coalescing or high-efficiency particulate filtration.
- Spatter particles: Larger molten droplets (10–500 µm) ejected from the melt pool. These are captured readily by standard particulate elements but can blind filter media quickly at high build rates.
- Soot and carbonaceous particles: Generated from residual binder in some powder feedstocks or from partial combustion of contaminants. Activated carbon adsorption is required to remove these.
- Moisture ingress: From powder loading, door seals, or gas supply lines. Even trace moisture (>10 ppm) can oxidise reactive metal powders such as titanium or aluminium alloys.
The recirculating gas — typically argon for titanium and reactive alloys, or nitrogen for stainless steel and tool steels — must be maintained at a purity level that protects both the build and the powder bed throughout the entire print cycle, which may last 24–72 hours for complex components.
Specifying the Filtration Train for Inert Gas Recirculation
A correctly specified filtration train for an SLM/DMLS recirculation loop typically comprises three stages, each addressing a distinct contamination class. The R+F process gas filter range provides housings and elements suited to each stage.
Stage 1 — Coarse Particulate Pre-Filter
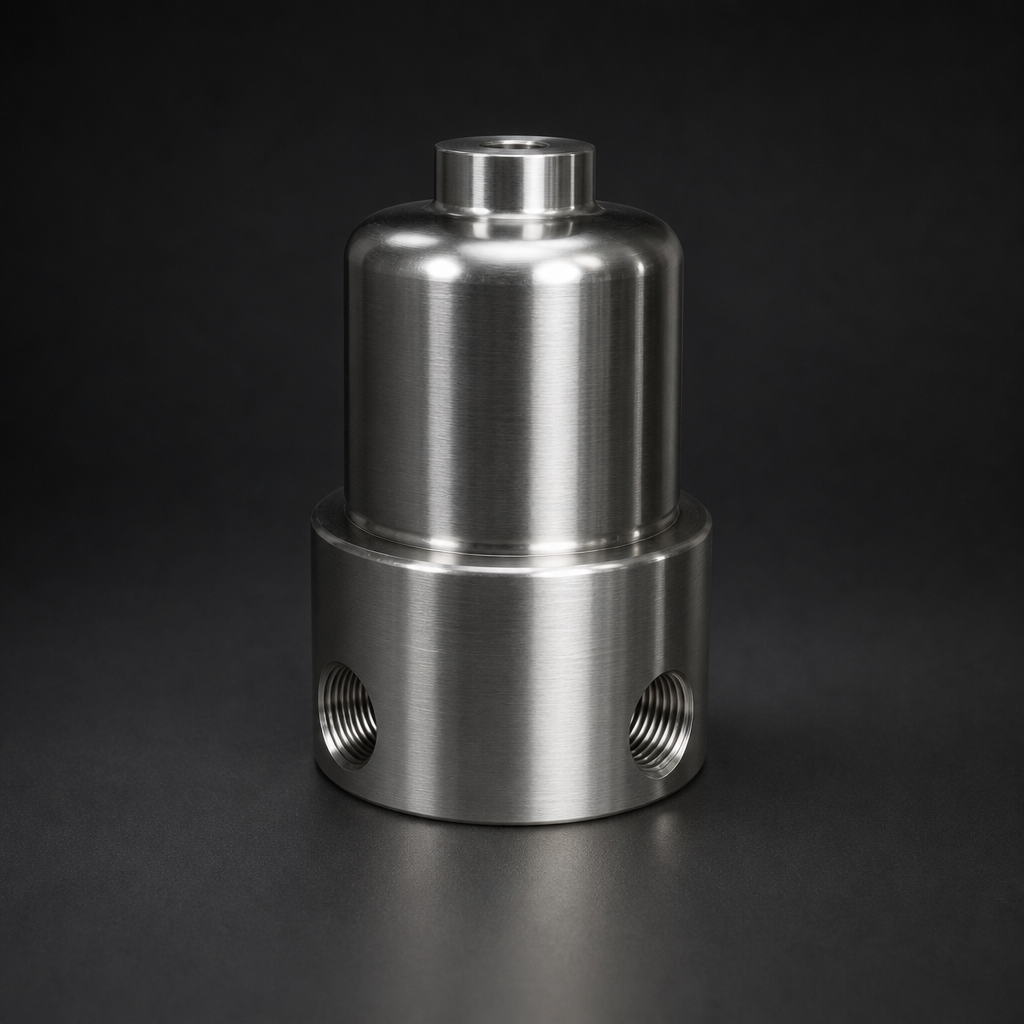
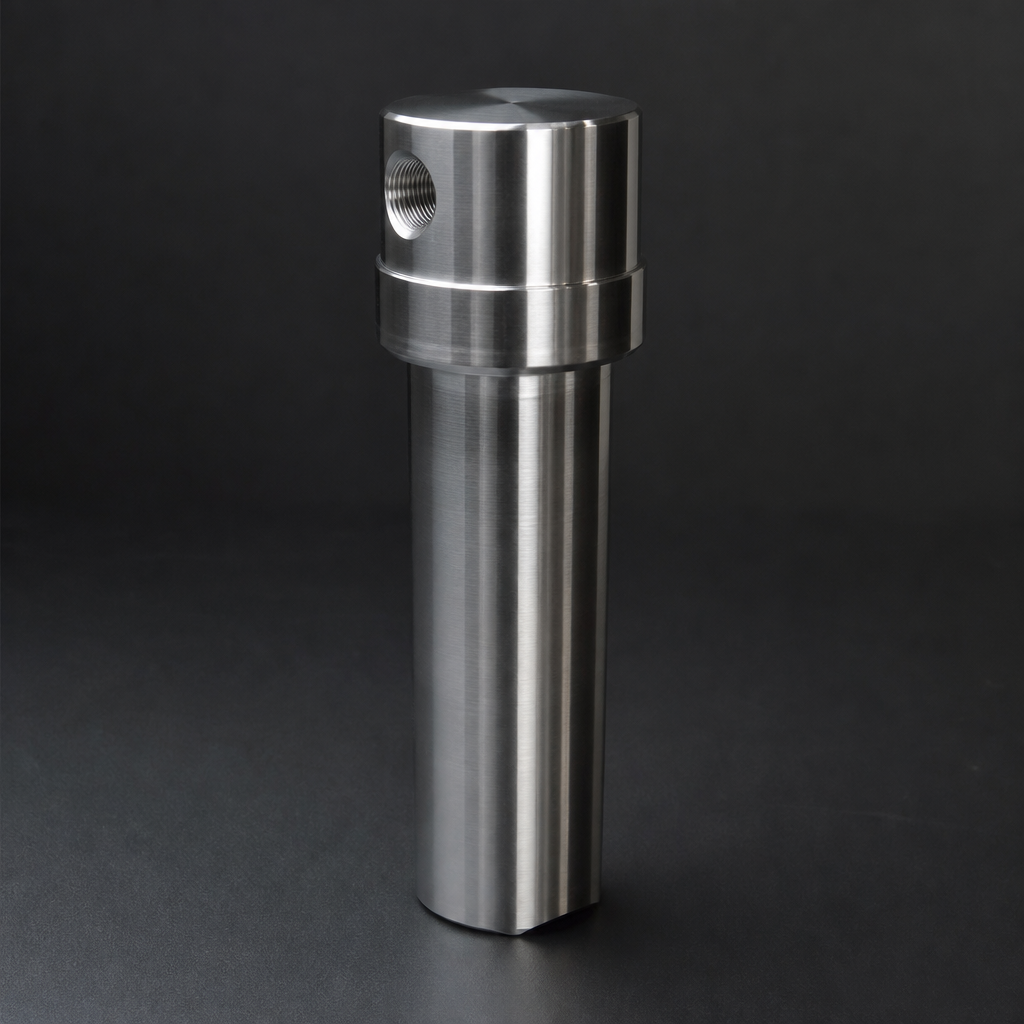
Spatter particles and larger agglomerates are captured at the inlet to protect downstream elements. An RF-DIL disposable inline filter is well suited here: its compact form factor allows installation close to the build chamber outlet, and its disposable design means contaminated elements can be replaced without exposing personnel to metal fume. For higher-flow systems, a RF-H-150 stainless steel housing fitted with an RF-P particulate element (99.99% efficiency ≥ 0.3 µm) provides robust pre-filtration at pressures up to 100 bar.
Stage 2 — High-Efficiency Coalescing / Sub-Micron Particulate Filter
Metal condensate fume — the most damaging contaminant for laser optics and build quality — is captured at this stage. The RF-C coalescing element, manufactured from borosilicate glass microfibre, achieves 99.99% efficiency at ≥ 0.1 µm. For argon recirculation systems operating at elevated pressure, the RF-H-150 housing in 316L stainless steel with FKM seals is the preferred choice, offering compatibility with argon and nitrogen at temperatures up to 200 °C with S-type elements.
Stage 3 — Activated Carbon Adsorption
Soot, hydrocarbons, and trace organic contaminants are removed by an RF-AC activated carbon element, reducing residual oil content to below 0.003 mg/m³. This stage is particularly important when the inert gas supply is drawn from cylinders that may carry trace compressor oil, or when the recirculation blower introduces hydrocarbon vapour. See our guide on coalescing vs particulate filter elements for a detailed comparison of element selection criteria.
Comparing Filtration Approaches for Additive Manufacturing
| Approach | Particle Removal | Hydrocarbon Removal | Suitability for Argon/N₂ | Maintenance |
|---|---|---|---|---|
| RF-DIL inline + RF-C coalescing + RF-AC adsorption | 99.99% ≥ 0.1 µm | <0.003 mg/m³ | Excellent (316L SS, FKM) | Element swap only |
| HEPA filter only | 99.97% ≥ 0.3 µm | None | Limited (housing materials vary) | Full unit replacement |
| OEM machine filter (built-in) | Varies (typically ≥ 1 µm) | None | Good (purpose-built) | OEM parts only, high cost |
| Electrostatic precipitator | High for fume | None | Poor (spark risk with argon) | Plate cleaning required |
Need help selecting the right filter for your additive manufacturing system?
Use our free Engineering Tool to get a filtration recommendation for your specific application in under 2 minutes.
Pressure Drop and Flow Rate Considerations
Recirculation blowers in SLM machines typically operate at low differential pressures (50–200 mbar) and moderate flow rates (50–500 Nm³/h depending on build volume). Excessive filter pressure drop reduces gas velocity across the powder bed, which can allow spatter to settle and contaminate unsintered powder. When selecting elements, always verify the pressure drop curve at your operating flow rate — the R+F Engineering Sizing Tool allows you to model pressure drop for RF-C and RF-P elements across the full flow range.
For larger industrial SLM systems with multiple build chambers operating in parallel, a centralised filtration skid using RF-H-150 housings in a manifold arrangement provides the most cost-effective solution, with individual element change-out possible without interrupting adjacent chambers.
- Metal condensate (fume):
- A correctly specified filtration train for an SLM/DMLS recirculation loop typically comprises three stages, each addressing a distinct contamination class.
- Recirculation blowers in SLM machines typically operate at low differential pressures (50–200 mbar) and moderate flow rates (50–500 Nm³/h depending on build volume).
Element Change Intervals and Monitoring
Unlike compressed air systems where differential pressure gauges provide reliable change-out indicators, inert gas recirculation filters in additive manufacturing are best managed on a build-count or operating-hour basis. Metal condensate loading is highly variable — titanium alloy builds generate significantly more fume than stainless steel — so a conservative approach is recommended. Typical intervals are 200–500 operating hours for the coalescing stage, with the activated carbon RF-AC element changed annually or when hydrocarbon breakthrough is detected by inline monitoring.
For further reading on gas purity standards and element selection, see our articles on ISO 8573-1 compressed air quality classes and hydrogen electrolysis filtration, which share many of the same purity requirements as inert gas AM systems.
Related Reading
- Coalescing vs Particulate Filter Elements — Which Do You Need?
- ISO 8573-1 Compressed Air Quality Classes Explained
- Oxygen Filtration Safety — What Engineers Need to Know
Try our Engineering Sizing Tool → or discuss your requirements with our team.