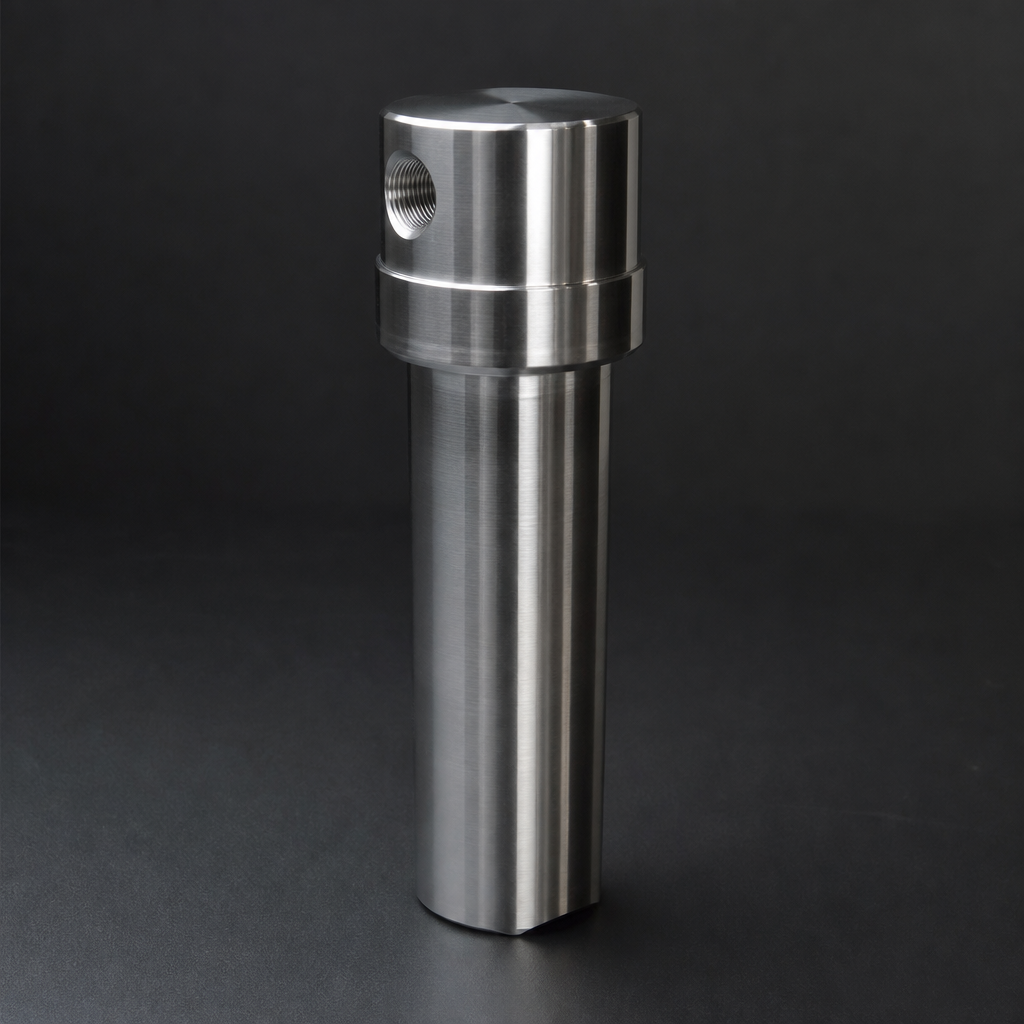
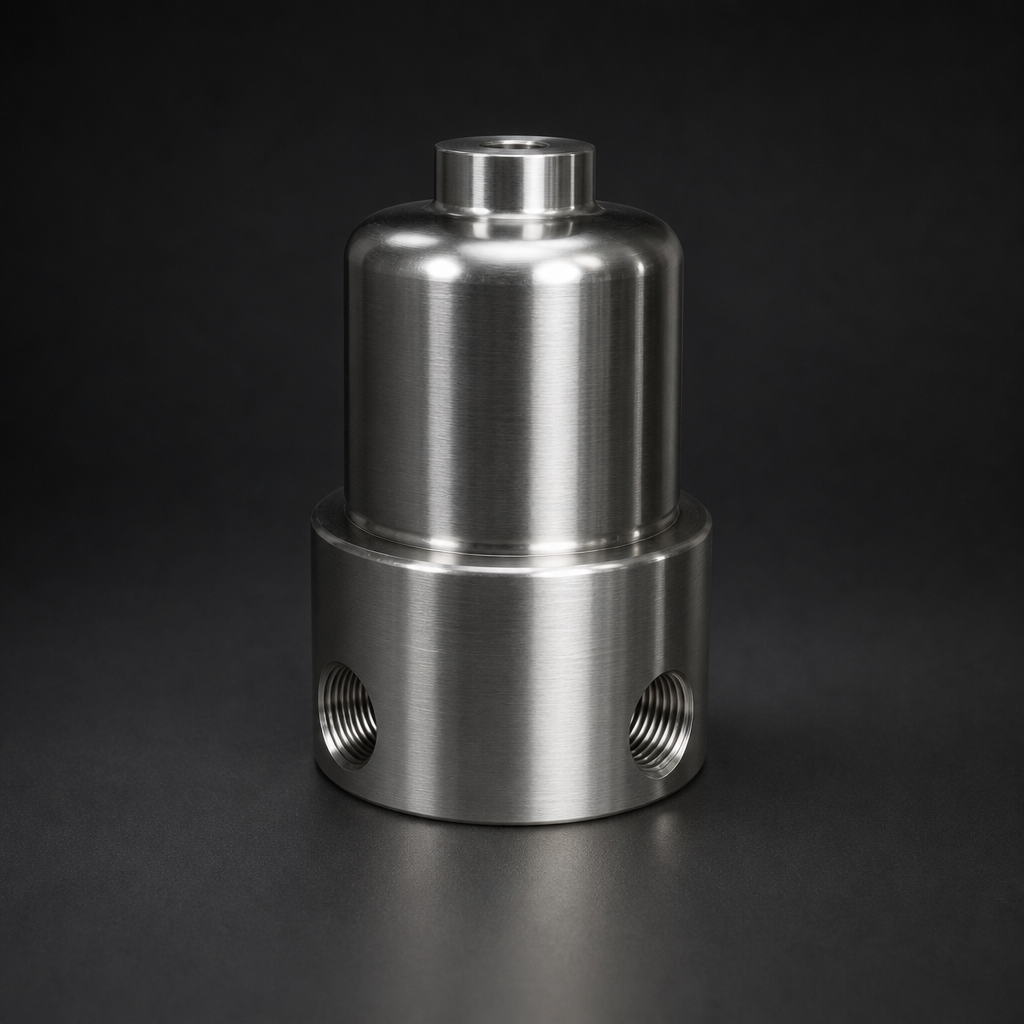
Liquid carry-over is one of the most damaging — and most preventable — failures in analytical instrumentation. When a coalescing filter housing floods, liquid migrates downstream and enters the analyser, causing costly damage, unplanned downtime, and potentially hazardous measurement errors. Float valve filter housings exist precisely to prevent this scenario, yet many engineers are unaware of how they work or when to specify them.
The Problem: What Happens When a Coalescing Housing Floods
In a typical instrumentation filter installation, a coalescing element captures liquid aerosols and bulk liquid from the sample gas stream. The separated liquid collects in the bowl at the bottom of the housing. Under normal operation, this liquid is drained periodically — either manually or via an automatic drain.
Problems arise when the drain fails, maintenance is delayed, or liquid loading is unexpectedly high. The bowl fills, liquid rises above the element, and the gas stream carries liquid droplets — or even a slug of liquid — directly into the downstream sample conditioning system and, ultimately, the analyser itself.
The root cause is straightforward: a standard coalescing housing has no mechanism to detect or respond to a rising liquid level. It simply passes whatever is in the bowl downstream once the liquid level reaches the outlet port.
Float Valve Housing Technology: How It Works
A float valve housing adds a liquid-level sensing and shut-off mechanism to the standard coalescing housing design. The operating principle is elegantly simple:
- Gas enters the housing and passes through the coalescing element. Separated liquid collects in the bowl as normal.
- A float assembly — typically a hollow stainless steel or polymer sphere — sits in the bowl. As liquid accumulates, the float rises with the liquid level.
- When the liquid level reaches a critical height, the float assembly engages a valve seat and closes the gas outlet port completely.
- Flow to the analyser stops. The sudden loss of sample flow triggers an alarm in the control system.
- The operator is alerted before any liquid reaches the analyser. The housing can be drained and returned to service without analyser damage.
This approach is particularly valuable in unattended or remote installations, where a flooded housing might go unnoticed for hours or days before the next manual inspection.
Where Float Valve Housings Are Specified
Float valve protection is most commonly specified in analytical instrumentation applications where the downstream equipment is expensive, sensitive, or difficult to replace. Typical installations include:
- Process gas chromatographs (GC) — where liquid contamination destroys columns and detectors
- Continuous emissions monitoring systems (CEMS) — where regulatory compliance depends on uninterrupted, accurate measurement
- Infrared and UV analysers — where liquid in the optical path causes immediate measurement failure
- Mass spectrometers — where liquid ingress can damage the vacuum system and ionisation source
- Moisture analysers — where liquid carry-over saturates the sensor and requires lengthy reconditioning
In each case, the cost of the float valve housing is trivial compared to the cost of analyser repair or replacement.
Continuous emissions monitoring systems (CEMS)
R+F FilterElements Analyser Protection Housings: The RF-H-170 Series
R+F FilterElements offers the RF-H-170 series of high-pressure analyser protection housings, designed specifically for demanding sample conditioning applications. These housings are available from R+F FilterElements in both standard and float valve configurations, covering a wide range of operating conditions.
The RF-H-170 series accepts standard R+F coalescing elements (RF-C series) and particulate elements (RF-P series), ensuring consistent filtration performance across the full operating range. For applications involving corrosive or ultra-pure gases, SilcoNert-coated variants are available from R+F FilterElements.
Use our free Engineering Tool to get a filtration recommendation for your specific application in under 2 minutes.
Material Selection: Stainless Steel vs. Engineered Polymer
Float valve housings are available in two primary material families, each suited to different application requirements:
| Parameter | 316L Stainless Steel | Engineered Polymer (Nylon / PP / PVDF) |
|---|---|---|
| Pressure rating | Up to 400 bar | Typically up to 10–16 bar |
| Temperature range | −40 °C to +200 °C (FKM seals) | −10 °C to +80 °C (typical) |
| Chemical resistance | Excellent (most process gases) | Good (non-oxidising, non-aromatic) |
| Typical applications | Process GC, CEMS, H₂S service, high-pressure sample lines | General laboratory, low-pressure utility gas, water treatment |
| Float material | 316L SS hollow sphere | Polypropylene or PVDF sphere |
| Relative cost | Higher | Lower |
For most process gas and analyser sample contamination prevention applications, 316L stainless steel is the correct choice. Polymer housings are appropriate for general-purpose laboratory or utility gas applications where pressures are low and the gas stream is non-aggressive.
Seal Selection for Float Valve Housings
Seal material selection is critical in float valve housings because the float assembly itself relies on a resilient seal to achieve positive shut-off. The wrong seal material will swell, harden, or fail to seat correctly, compromising the protection function entirely.
R+F FilterElements supplies the RF-H-170 series with the following seal options:
- NBR — general-purpose hydrocarbons, up to 100 °C
- FKM/Viton — aggressive hydrocarbons, H₂S, CO₂, up to 200 °C
- EPDM — oxygen service (never use NBR or FKM with O₂)
- PTFE — ultra-pure and highly corrosive applications, up to 260 °C
Always specify the seal material based on the actual process gas composition, not just the nominal service. A natural gas application with significant H₂S content, for example, requires FKM rather than NBR to prevent premature seal degradation and float valve failure.
For further guidance on filter selection for process gas applications, see our guide to coalescing vs. particulate filter elements and our overview of process gas filter housings.
Installation and Maintenance Considerations
Float valve housings require the same installation care as standard coalescing housings, with a few additional points:
- Orientation — the housing must be installed vertically with the bowl downward. The float mechanism relies on gravity and will not function correctly in any other orientation.
- Drain provision — a manual or automatic drain must still be fitted. The float valve is a safety backup, not a substitute for regular draining.
- Alarm integration — the loss-of-flow signal must be connected to the plant DCS or analyser management system. A float valve that shuts off but raises no alarm provides no benefit in an unattended installation.
- Element replacement — coalescing elements should be replaced on schedule. A heavily loaded element increases differential pressure and reduces flow, which can mask the float valve shut-off signal.
Explore the full range of instrumentation and analyser protection filters available from R+F FilterElements, or use the Engineering Sizing Tool to select the correct housing and element combination for your application.
- In a typical instrumentation filter installation, a coalescing element captures liquid aerosols and bulk liquid from the sample gas stream.
- A float valve housing adds a liquid-level sensing and shut-off mechanism to the standard coalescing housing design.
- Process gas chromatographs (GC)
- R+F FilterElements offers the RF-H-170 series of high-pressure analyser protection housings, designed specifically for demanding sample conditioning applications.
Related Reading
- Coalescing vs. Particulate Filter Elements — Which Do You Need?
- ISO 8573-1 Compressed Air Quality Classes Explained
- Oxygen Filtration Safety — Why Standard Filters Are Not Enough
Try our Engineering Sizing Tool → or discuss your requirements with our team.