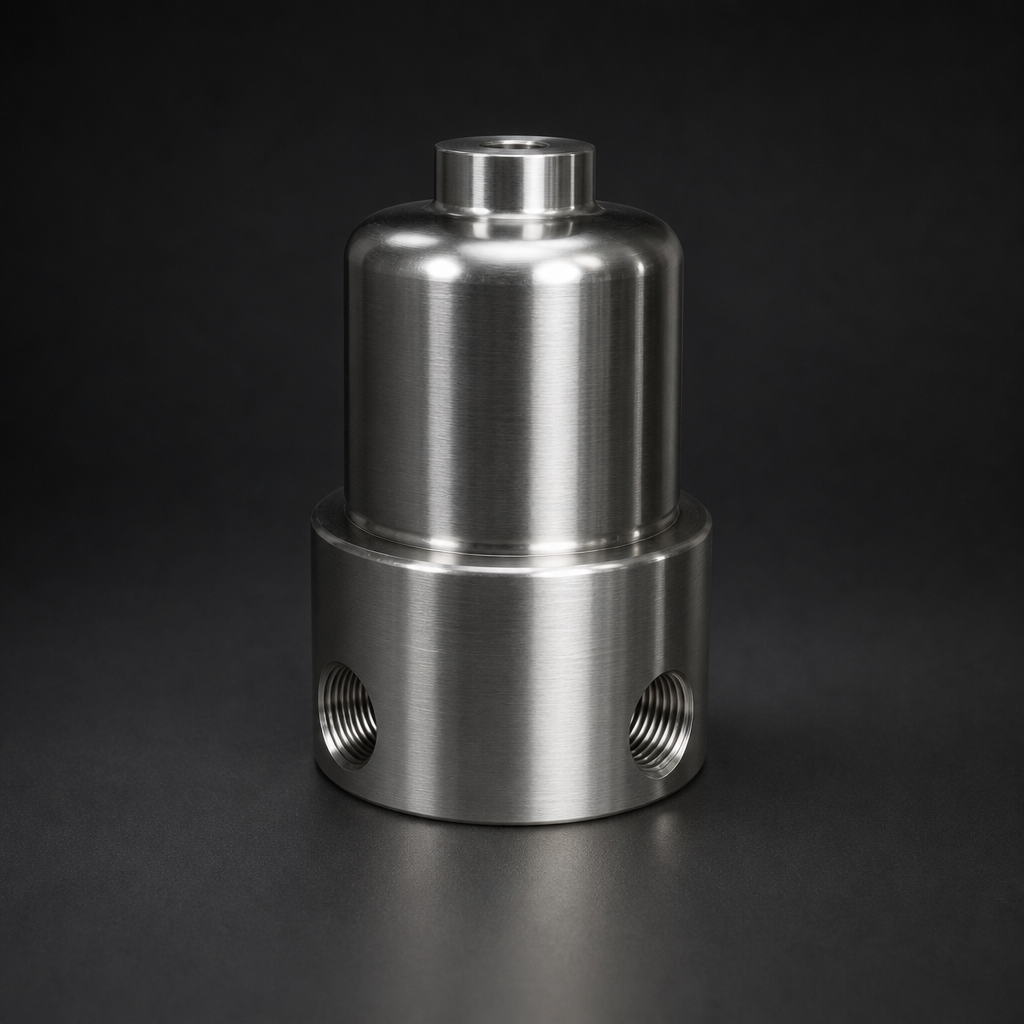
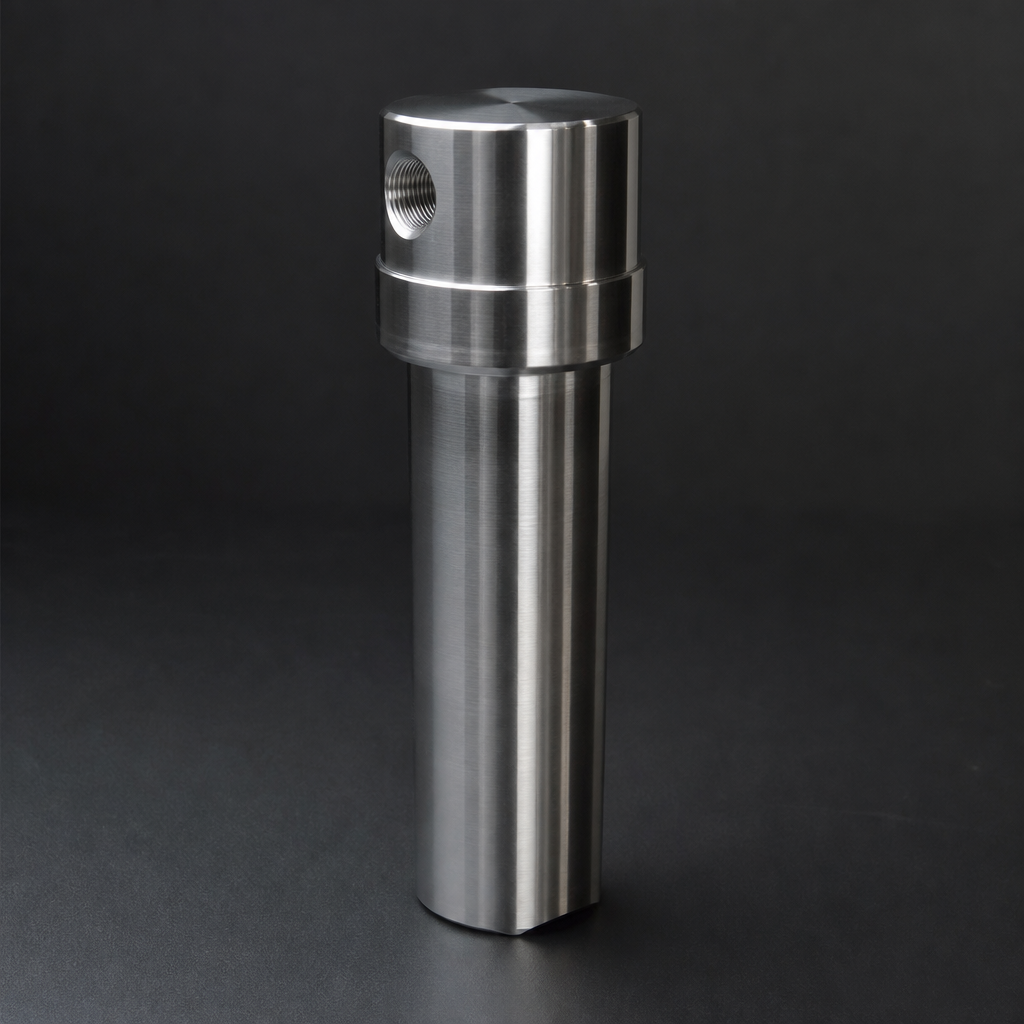
Diesel fuel, crude condensate, and liquid hydrocarbon samples drawn from process lines carry dissolved and free water that can wreck analyser cells, block sample conditioning trains, and produce false readings within minutes of start-up. Conventional coalescing filters designed for gas-phase duty are ineffective here: liquid hydrocarbons flood the element, water passes straight through, and the housing fills with a two-phase emulsion that is almost impossible to drain cleanly. The answer is a hydrophobic PTFE membrane separator — a device that exploits surface-tension physics to pass liquid hydrocarbons freely while forming an absolute barrier to water, regardless of flow rate or pressure fluctuation.
This guide explains how PTFE membrane water removal works, what to look for in a membrane housing, and how R+F FilterElements' RF-GMS-170 membrane separator and supporting instrumentation-grade housings solve the problem in diesel and liquid hydrocarbon sample conditioning systems.
Why Water in Diesel Samples Is a Persistent Problem
Diesel and liquid hydrocarbon streams are rarely dry. Condensation during transport, water ingress at storage tanks, and dissolved water released as temperature drops all contribute to a sample that can contain anywhere from a few hundred ppm to several percent free water by volume. When that sample reaches an online analyser — a near-infrared spectrometer, a viscometer, or a flash-point tester — even trace free water causes:
- Optical cell contamination and baseline drift in NIR and UV instruments
- Viscosity measurement errors of 5–15% in water-contaminated samples
- Premature corrosion of stainless steel sample lines and valve seats
- Emulsion formation that blocks fine-bore tubing and sample probes
The Membrane Separation Principle
A PTFE membrane separator works on the Laplace pressure equation: the pressure required to force a liquid through a pore is inversely proportional to the pore radius and directly proportional to the liquid's surface tension and the contact angle with the membrane material. For water on PTFE, the contact angle exceeds 110°, producing a bubble-point pressure far above any realistic sample line pressure. Liquid hydrocarbons, with their lower surface tension and near-zero contact angle on PTFE, pass through the same pores at pressures as low as 0.1 bar differential.
In practice, the membrane is supported on a sintered or woven backing layer to prevent mechanical collapse under pressure cycling. The flow path is designed so that the hydrocarbon sample contacts the upstream face of the membrane, permeates through, and exits to the analyser, while any free water accumulates on the upstream face and drains to a low-point drain or level-controlled dump valve.
Support Layers and Flow Path Design
The membrane alone is fragile — typically 50–200 µm thick — and must be laminated to a support structure that provides mechanical integrity without restricting flow. R+F FilterElements' RF-GMS-170 membrane separator uses a multi-layer construction:
- Upstream face: expanded PTFE (ePTFE) membrane, 0.2 µm nominal pore size
- Support layer: sintered 316L stainless steel disc, 10 µm nominal, providing structural rigidity up to 170 bar
- Downstream face: open-channel flow path machined into the 316L SS body, directing permeate to the outlet port
The housing body is machined from solid 316L stainless steel bar stock, with all wetted surfaces electropolished to Ra ≤ 0.4 µm. This matters for diesel and hydrocarbon samples because rough surfaces trap heavy fractions and create dead volumes that distort sample composition between analysis cycles. The RF-GMS-170 is rated to 170 bar working pressure, making it compatible with high-pressure sample take-off points on refinery process lines.
Need help selecting the right filter for your diesel or hydrocarbon sample conditioning system?
Comparing Water Removal Technologies for Liquid Hydrocarbon Samples
| Technology | Water Rejection | Pressure Rating | Maintenance | Surfactant Tolerance |
|---|---|---|---|---|
| PTFE Membrane (RF-GMS-170) | Absolute (100%) | Up to 170 bar | Membrane replacement only | Low (<50 ppm) |
| Coalescing filter (gas-phase) | Poor (floods in liquid) | Up to 700 bar (RF-H-170) | Element + drain | Moderate |
| Gravity separator / knock-out pot | Partial (free water only) | Vessel-rated | Level control, drain | Good |
| Molecular sieve adsorber (RF-DIA) | Dissolved water only | Up to 350 bar | Sieve replacement | Good |
Use our free Engineering Tool to get a filtration recommendation for your specific application in under 2 minutes.
Integrating the RF-GMS-170 into a Sample Conditioning Train
For a typical diesel analyser sample conditioning system, R+F FilterElements recommends a two-stage approach. The first stage uses an RF-H-150 process gas housing fitted with a 10 µm sintered metal element to remove particulate contamination — wax crystals, rust, and pipe scale — that would otherwise blind the membrane. The second stage is the RF-GMS-170 membrane separator, which provides the absolute water barrier. This sequence protects the membrane from abrasive damage and extends its service life significantly.
For samples with high dissolved water content (above 500 ppm), a pre-heating stage to 40–60 °C upstream of the membrane can improve permeation rate and reduce the risk of wax precipitation blocking the upstream face. The RF-GMS-170 housing is rated to 150 °C continuous service with PTFE seals, so this is well within its operating envelope.
Where the sample also contains light hydrocarbon vapours or dissolved gas, consider adding an RF-DIL inline particulate filter downstream of the membrane separator to catch any fine PTFE fibres that may shed during initial commissioning. This is a precautionary measure — the RF-GMS-170 membrane is mechanically robust — but it is good practice in high-value analyser protection applications.
For a full overview of sample conditioning filter selection, see our guide to coalescing vs particulate filter elements and the ISO 8573-1 compressed air quality guide, which covers the purity classes relevant to instrument supply gas used in sample conditioning systems.
Specifying the Right Membrane Housing
When specifying a PTFE membrane separator for diesel or liquid hydrocarbon duty, the key parameters to confirm are:
- Maximum working pressure: The RF-GMS-170 is rated to 170 bar, covering most refinery sample take-off pressures. For higher-pressure applications up to 400 bar, the RF-H-170 high-pressure housing with a custom membrane insert is available from R+F FilterElements.
- Sample flow rate: Membrane permeation rate is a function of membrane area and differential pressure. The RF-GMS-170 is sized for typical analyser sample flows of 0.5–5 L/h. Higher flows require a larger membrane area or parallel units.
- Temperature: PTFE seals handle up to 260 °C; the 316L SS body is rated to 200 °C continuous. FKM/Viton seals are available for intermediate temperatures where PTFE is not required.
- Connection size: Standard 1/4" and 1/2" NPT or compression fittings; Swagelok-compatible tube fittings available on request.
- Diesel and liquid hydrocarbon streams are rarely dry.
- A PTFE membrane separator works on the Laplace pressure equation: the pressure required to force a liquid through a pore is inversely proportional to the pore radius and directly proportional to the liquid's surface tension and the contact angle with the membrane material.
- The membrane alone is fragile — typically 50–200 µm thick — and must be laminated to a support structure that provides mechanical integrity without restricting flow.
- For a typical diesel analyser sample conditioning system, R+F FilterElements recommends a two-stage approach.
Related Reading
- Coalescing vs Particulate Filter Elements — Which Do You Need?
- Filtration for Hydrogen Electrolysis Systems
- Oxygen Filtration Safety — What Every Engineer Should Know
Try our Engineering Sizing Tool → or discuss your requirements with our team.